How Metal Stamping Parts Are Made: From Steel Coil to Finished Product
In our system, we do not process parts in stages. Instead, we continuously shape them on a stable production line. Overall, we refine and gradually form each part. This process continues until they become finished products.
Below is the actual manufacturing process in our factory. It follows the part from steel coil to finished product.
Engineering and Tooling Preparation
Before each project begins, we enter the drawings into the engineering system for verification. The engineering team focuses on whether the structure is suitable for mass production, for example:
- Is it suitable for a continuous stamping structure?
- Does the material thickness stay stable and well formed?
- Do the hole positions and bending affect the mold’s lifespan?
- The risk of consistency in mass production
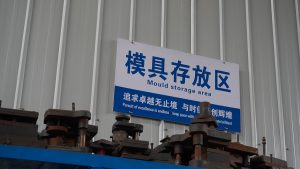
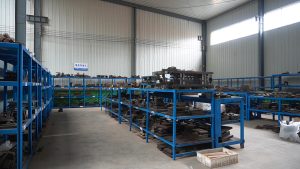
After we confirm the direction, the tooling enters the design and processing stage.In a metal stamping project, tooling determines part shape. It also affects production stability and batch consistency. Once the tooling enters production, it affects every part that follows.A single tool may produce tens of thousands or even hundreds of thousands of parts.
Metal Stamping Production Process
Consequently, the steel coils enter the stamping production line via the feeding system, and production immediately enters continuous operation.
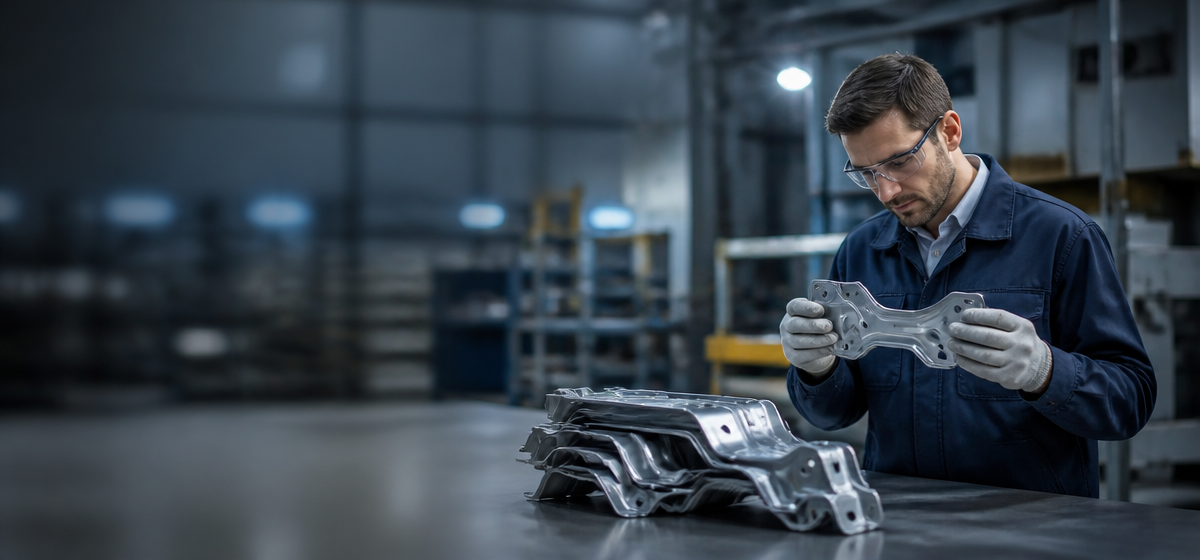
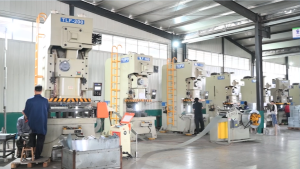
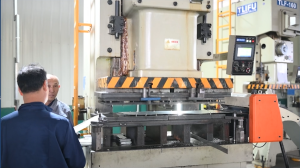
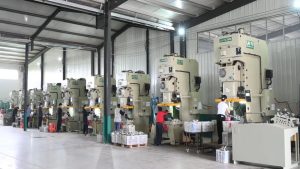
In the workshop, 40 stamping machines operate simultaneously.Different products run continuously on separate production lines.In continuous die production, the steel strip moves through multiple stations.Each station performs a specific operation until the part takes full shape.
• The shape gradually takes shape
• The hole positions appear simultaneously
• The local structure gradually takes shape
• Finally, the overall outline takes shape
For high-volume projects, we use progressive dies. Thus, these dies complete multiple operations in one production cycle. Meanwhile, the steel strip advances through each station. During this movement, cutting, piercing, forming, and bending happen progressively. Finally, the finished part exits the die at the end.
The entire process ran at a high-speed rhythm, with the equipment running almost continuously. During mass production, the key controls focused on mold stability, batch consistency, the range of size variations, and the continuous stamping rhythm. This is also the core advantage of metal stamping – achieving high efficiency and high consistency simultaneously.
Batch consistency
Size fluctuation range
Continuous stamping cycle
Secondary Manufacturing Operations
After stamping, the metal parts will follow different post-processing paths depending on the product structure.
• Some parts require edge treatment to make them suitable for assembly and use.
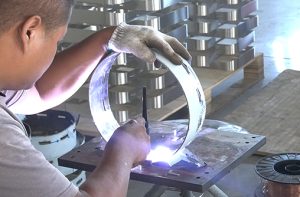
• Some structural components will enter the welding area and complete the connection of the combined structure within the production line. Overall, we plan each path before the job starts.
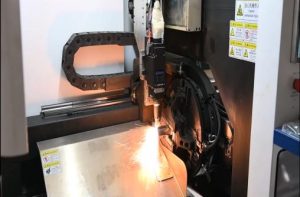
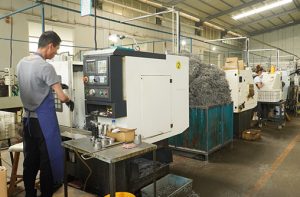
• Parts that require higher precision or additional structures will enter the CNC processing equipment for supplementary processing.
In our production system, we complete all these processes in the same factory, ensuring a continuous flow of parts between them.
One pressing family that forms under different logic is deep drawing — the full explanation is in our guide What Is Metal Deep Drawing? A Complete Manufacturing Guide.
Surface Finishing
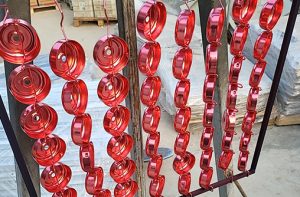
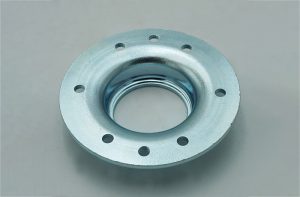
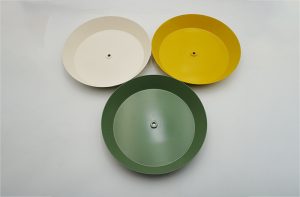
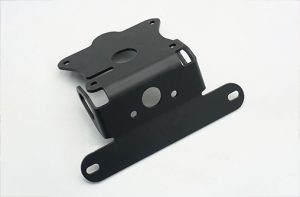
After we complete the structural processing, the parts enter the surface treatment stage. On the production line, we send the parts in batches to different treatment systems, and we optimize their functions according to the usage environment:
| Outdoor environment → Powder coating to enhance corrosion resistance |
Stainless steel parts → Passivation to improve oxidation resistance |
Appearance components → Electroplating or polishing |
The main objective of this stage is not merely about the appearance changes, but also about making the parts adapt to the actual usage environment.
Quality Control System
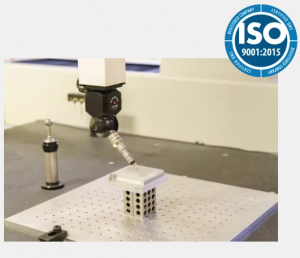
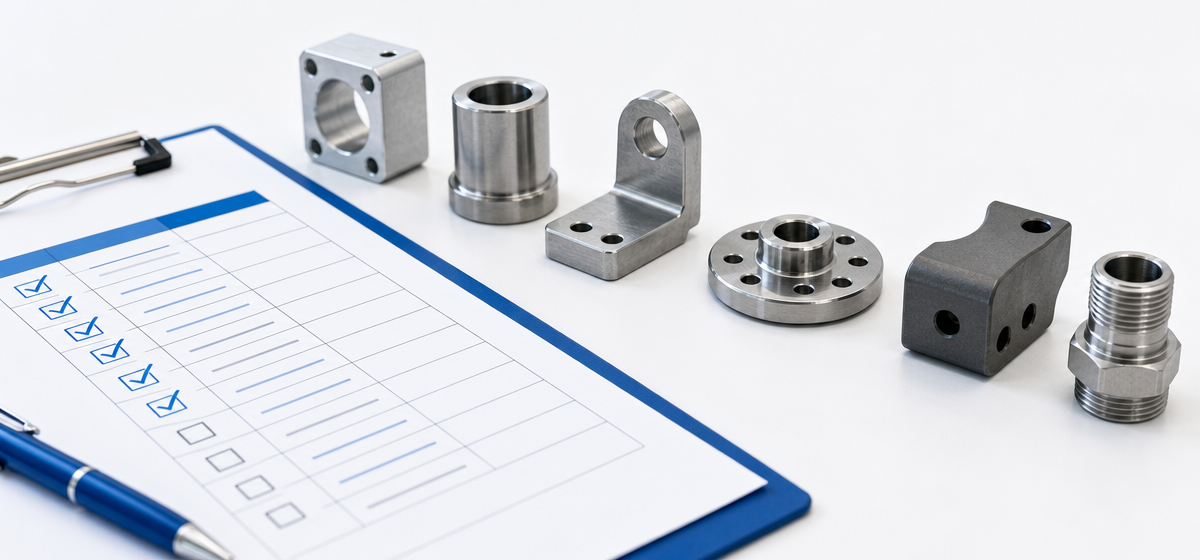
In metal stamping, quality control is not a final check. Instead, it is a continuous mechanism. It runs throughout the entire production process.
• At production start, we confirm the first piece. This ensures the tooling matches the drawing.
• During mass production, we conduct sampling inspections. Meanwhile, we focus on key dimensions. This helps us monitor overall stability.
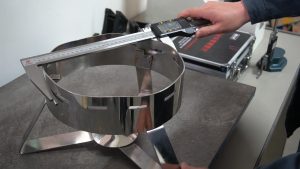
• For complex structural parts, we use coordinate measuring equipment. This verifies dimensional accuracy.
Overall, from incoming material inspection to final shipment verification, we integrate quality checkpoints throughout production to maintain batch consistency and dimensional accuracy.
One-stop Metal Stamping Manufacturing System
In some manufacturing models, stamping, welding, machining, and surface treatment often run separately in different supply chains. However, in our production system, these processes run continuously within the same factory:
The direct results of this structure are: a more continuous production rhythm, more stable batch quality, better control over delivery cycles, and shorter communication links. For batch purchasing projects, the integrated model can significantly reduce overall manufacturing risks.
One-Stop Metal Stamping Manufacturing
The formation of a metal stamping part is not the result of a single operation, but the outcome of the continuous operation of the entire production line. After the steel coil enters the production line, the tooling and equipment work in coordination to continuously transform it into a structurally stable metal part.
We have manufactured more than 70,000 metal parts for customers worldwide. Overall, backed by an experienced engineering team and stamping equipment, we provide reliable one-stop metal-stamping services.
Frequently Asked Questions
Q1. What happens between the steel coil and the finished stamped part?
We load the coil into the feeding system, and it enters continuous stamping, where the die cuts and forms the part in one pass of the line. After stamping, parts follow the post-processing path their structure requires, such as edge treatment, additional machining or welding, and then surface finishing. Quality control runs alongside production instead of only at the end. Because stamping, welding, machining, and surface treatment happen continuously inside one system, batches stay consistent rather than moving between separate supply chains.
Q2. What does the engineering team check before a stamping project starts?
Before production, we enter the drawings into the engineering system and verify them against continuous, high-volume production. The team checks whether the structure suits a continuous die, how we should arrange the stations, and where forming or tolerance issues could appear once the tool is running in the workshop. This review happens before we build the tooling, because the decisions we take at this stage determine tool life, scrap rate, and whether the process stays stable from the first piece to the last.
Q3. How is quality controlled during metal stamping?
Quality control is a continuous mechanism rather than a final inspection. At the start of production we confirm the first piece so the tooling matches the drawing, and during the run we check parts at set intervals while we monitor process parameters so we catch drift early. Because stamping, welding, machining, and surface treatment all run in the same facility, one quality system follows the part through every stage, and final inspection confirms dimensions instead of discovering the problem.
Frequently Asked Questions
Q1. What happens between the steel coil and the finished stamped part?
We load the coil into the feeding system, and it enters continuous stamping, where the die cuts and forms the part in one pass of the line. After stamping, parts follow the post-processing path their structure requires, such as edge treatment, additional machining or welding, and then surface finishing. Quality control runs alongside production instead of only at the end. Because stamping, welding, machining, and surface treatment happen continuously inside one system, batches stay consistent rather than moving between separate supply chains.
Q2. What does the engineering team check before a stamping project starts?
Before production, we enter the drawings into the engineering system and verify them against continuous, high-volume production. The team checks whether the structure suits a continuous die, how we should arrange the stations, and where forming or tolerance issues could appear once the tool is running in the workshop. This review happens before we build the tooling, because the decisions we take at this stage determine tool life, scrap rate, and whether the process stays stable from the first piece to the last.
Q3. How is quality controlled during metal stamping?
Quality control is a continuous mechanism rather than a final inspection. At the start of production we confirm the first piece so the tooling matches the drawing, and during the run we check parts at set intervals while we monitor process parameters so we catch drift early. Because stamping, welding, machining, and surface treatment all run in the same facility, one quality system follows the part through every stage, and final inspection confirms dimensions instead of discovering the problem.
Need a Reliable Metal Stamping Manufacturer?
✅ Continuous stamping · Stable batch production · On-time delivery
📩 tylor@xinjiuxinji.com — We respond to inquiries within 2 hours.
Contact us today for a free feasibility review & quote — Send your drawings now
Stainless Steel Fabrication: Materials, Processes and RFQ