How Does a Steel Fabrication Factory Work? A Behind-the-Scenes Look
Picture a drawing in your hand, with a steel part on it. You also know the material, the size, and the tolerances it needs. But what happens after the drawing reaches the factory workshop?
Steel Fabrication is not as simple as cutting the steel plate and then welding it together. So in our factory, from drawing review to final delivery, the product moves through multiple collaborative steps. Technical review, material preparation, cutting, shaping, welding, surface treatment, inspection, packaging, and shipping each follow their own standards and procedures.
This article takes you through the complete process in a steel fabrication factory. It’s not a conceptual introduction, but rather what happens every day in the workshop.
What Happens After a Drawing Reaches the Factory?
When a drawing arrives, it doesn’t go straight to the workshop.
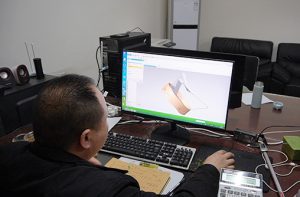 Our engineering team starts with a drawing review. They assess whether our current equipment and processes can produce the part consistently. They also identify the most efficient approach and any potential quality risks.
For example, if a certain bending angle is too small, making it according to the drawings might cause cracking. The engineering team flags it and suggests adjustments during the quoting stage. If a tolerance is too strict to hold in production, they note it and confirm how to relax it. They can also optimize the cutting layout of a certain part and lift the steel utilization rate from 75% to over 90%. So this is another opportunity the drawing stage reveals.
We call this stage DFM (Design for Manufacturing) assessment. Our 19 engineers go through the drawings from beginning to end before the project starts.
After the drawing review passes, we decompose the three-dimensional models into the two-dimensional unfolded diagrams of each part. We also generate the processing programs for the laser cutting and CNC machines. Then we issue the production instructions to the workshop.
Raw Material Inspection and Pre-Treatment
So steel plates, steel sections, and pipes arrive from the steel mill first. They do not enter the workshop for direct cutting.
First, quality inspectors conduct incoming material inspection. Specifically, they verify the material grade and specification size against the purchase order. They also check for defects such as rust, cracks, or surface blemishes. Then we archive the quality certification documents for each batch of raw materials. So we can trace every finished product back to the source of its raw materials.
Qualified materials then proceed to the pre-treatment stage. So only steel plates with clean surfaces can enter the cutting process. Rust and oil stains would affect the cutting quality and the stability of subsequent welding.
Laser Cutting in Steel Fabrication — Transforming Plate into Parts
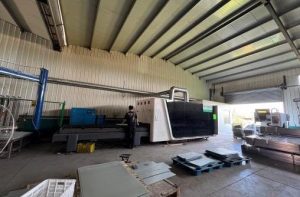 So the large sheets of steel move to the cutting platform, and the numerical control system runs the cutting on the program we prepared earlier. So our equipment covers the cutting needs of different thicknesses and precision levels.
Specifically, we run 2 sets of 6-kw laser cutting equipment for high-precision work on medium and thin plates. The cuts come out smooth, with small heat zones and tighter tolerance control than plasma or flame cutting. For parts that need subsequent welding or bending, the laser-cut edges go straight to the next process, without secondary trimming.
After cutting, we direct the parts to different stations based on their types. Some go straight to stamping or bending, some enter the welding area, and some need further CNC machining.
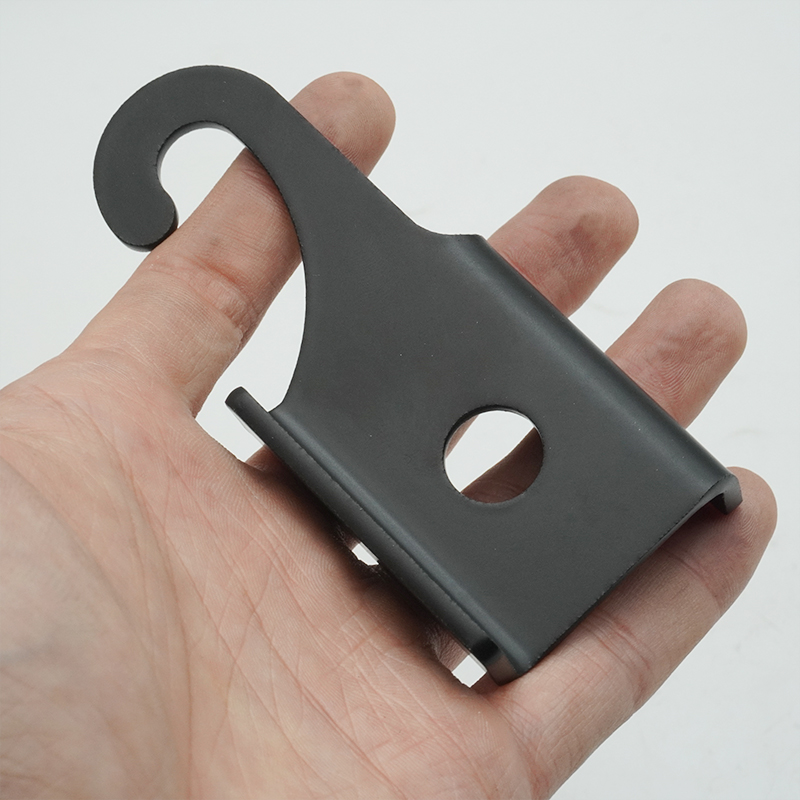
Forming – Stamping, Bending, and Deep Drawing
But not all parts are flat.
Parts that need bending or shaping enter the forming process next. At this stage, the equipment stays concentrated:
40 sets of 80-400 ton stamping machines cover thin sheets to medium-thick plates. We install the molds on the stamping machines. Then the plates go through one or multiple stamping processes, and the presses form the required concave and convex shapes. For deeper, more complex cup-shaped or box-shaped parts, we use the deep drawing process. The flat material then becomes a three-dimensional shape through multiple stretch operations.
3 sets of bending machines handle the bending and forming of pipes and profiles. 4 sets of hydraulic presses cover the forming and correction operations that require greater pressure.
The key to the forming process is controlling the rebound. So after we bend the steel plate, it slightly rebounds. At a 90-degree bending angle, it may become 91 degrees when released. Our technicians compensate the rebound amount in the programming, based on material grade and thickness. So the final dimensions meet the drawing requirements.
For high-precision milling, parts pass through the CNC milling machine, five-axis CNC machining center, and vertical machining center. Then the machine tools complete the final fine processing of the dimensions.
Welding and Assembly
Many steel fabrication products take their final form through welding multiple parts together.
Welding is one of the most technically demanding steps. Welder qualifications, parameters, filler metal selection, and environmental conditions—every variable affects weld quality.
Before welding, fitters perform tack-up—positioning and temporarily tack-welding parts according to the drawing, then verifying key dimensions. Only after dimensional confirmation do they proceed to final welding.
Our welding equipment includes one automatic spot welder and three welding production lines. Automated welding has clear advantages in volume production: stable parameters, consistent speed, and minimal human variation. That makes it ideal for repeatable parts. Manual welding remains more flexible for small batches or complex geometries.
After welding, a critical step follows: straightening. Heat from welding distorts steel, and the finished weldment may have shifted from its original shape. Mechanical or flame straightening brings dimensions back within tolerance.
Why does surface treatment matter for steel parts?
So after welding and shaping, the parts achieve the shape that the drawings require. However, steel exposed to the air will rust, so most products still need surface treatment.
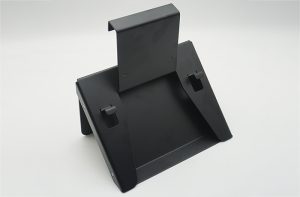
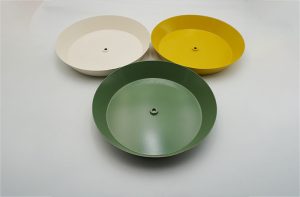
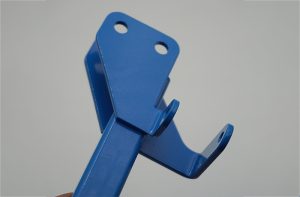
So our two surface treatment production lines cover a variety of process routes. Shot blasting or sandblasting removes oxide layers and welding spatter, and it builds the roughness that coating needs. Also, liquid spraying (epoxy primer + polyurethane topcoat) and powder coating meet different appearance and weather resistance requirements. Dactyl coating and galvanizing suit high-corrosion scenarios, while blackening serves internal components without thick coating protection. We choose the specific scheme based on the product’s usage environment and customer requirements.
Then the four sets of laser marking machines mark trace codes, specification parameters, or brand logos on the products. They do this without damaging the coating, and the content stays permanently clear.
Where Does Quality Inspection Happen in the Process?
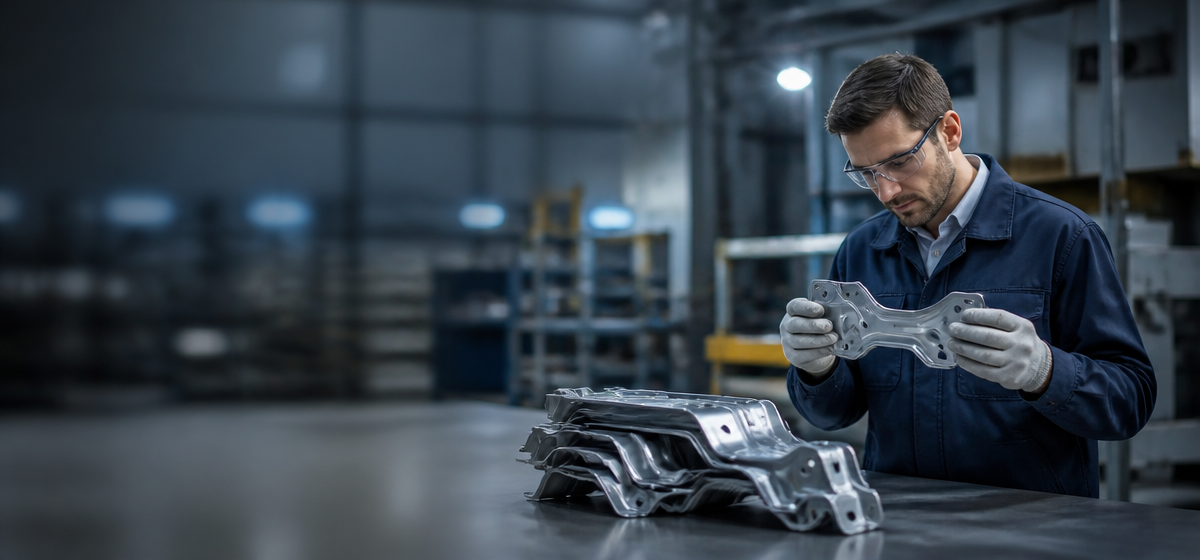
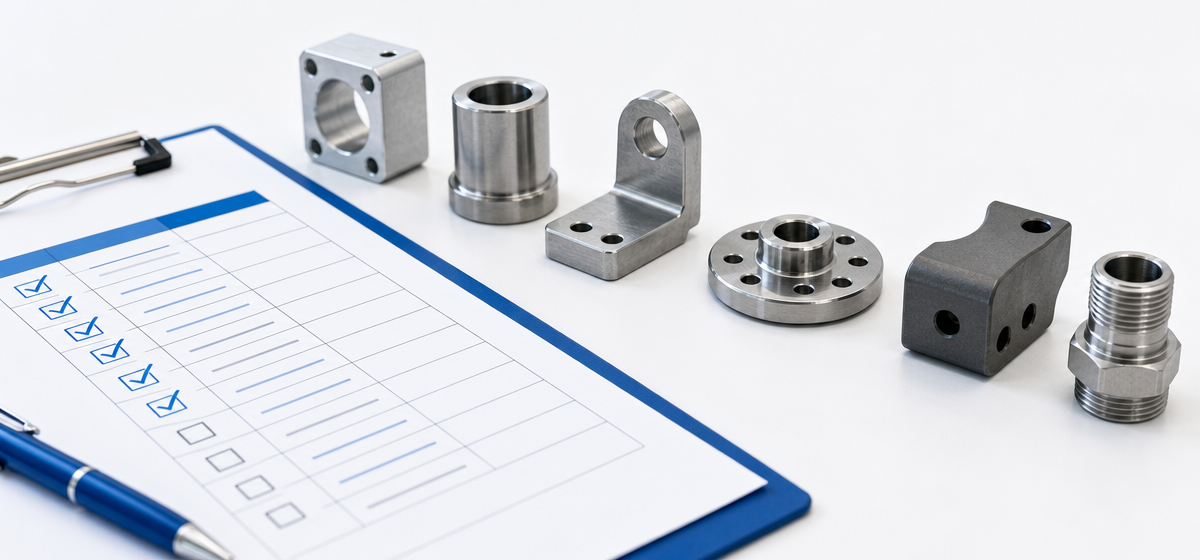
Quality inspection is not the final step; it runs through the entire production process.
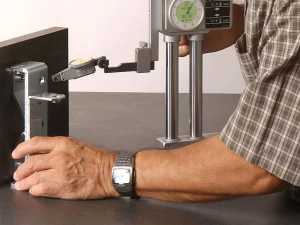 Our coordinate measuring machine (CMM) can quickly inspect complex parts. For parts with high tolerance requirements, CMM is the core tool to ensure batch consistency.
Incoming material inspection: Confirm the material and surface quality when raw materials arrive at the factory.
Process inspection: Random inspection of cutting dimensions, verification of forming dimensions, and inspection of weld appearance during the welding process.
Finished product final inspection: comprehensive checks of all dimensions, non-destructive weld testing when necessary, and paint film thickness measurement.
Each batch of products has corresponding quality inspection records. These records confirm final quality before shipment and back quality traceability. We also provide a quality inspection report for each batch of shipments.
Packaging and Shipping
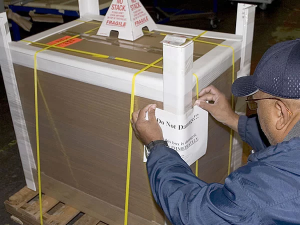 The qualified products then proceed to the packaging stage.
So steel fabrication products are often heavy, and they take irregular shapes. Shipping impacts and friction can cause surface damage. We tailor each packaging solution to the product. Specifically, we address three factors: secure tie-down, protective padding, and moisture barriers. The tie-down prevents transit movement, the padding prevents dents and scratches, and the barriers prevent ocean-shipping rust.
With mature international logistics experience, we have shipped over 70,000 different part types to 3,000+ customers across 100+ countries. Our stable daily output exceeds 50,000 parts, supported by fully automated, round-the-clock production.
From Drawing to Finished Steel Parts — One-Stop Fabrication in China
✅ DFM-driven engineering · In-house cutting, welding & finishing · On-time delivery
📩 tylor@xinjiuxinji.com — We respond to inquiries within 2 hours.
Send your drawings today for a free feasibility review & accurate cost estimate
Frequently Asked Questions
What are the main steps in a steel-fabrication project?
A typical project moves from drawing and requirement review to material planning, process planning, fabrication, welding or secondary operations, inspection, surface treatment when required, packaging, and delivery. The actual route depends on the part and its quality requirements.
How does a factory control batch-to-batch consistency?
Consistency depends on an approved drawing and process route, controlled material and tooling, defined inspection points, documented records, and traceability. These controls should be agreed before production rather than added after a problem appears.
What information should a buyer provide before production review?
Provide the current drawing revision, material and thickness, quantity, tolerance, finish, inspection requirements, packaging expectations, destination, and any critical characteristics. Clear inputs reduce assumptions during process planning.
How are projects with multiple processes coordinated?
The factory should define the process sequence, handoff points, fixtures or tooling, inspection responsibilities, and records for each stage. Coordinating the sequence helps control dimensional changes, surface condition, and delivery timing. The machines these routes run on are itemized, with their specifications, on our equipment list page.
How to Choose a China Sheet Metal Fabrication Manufacturer: The 2026 Buyer’s Guide